Polishing
Precision begins at the surface.
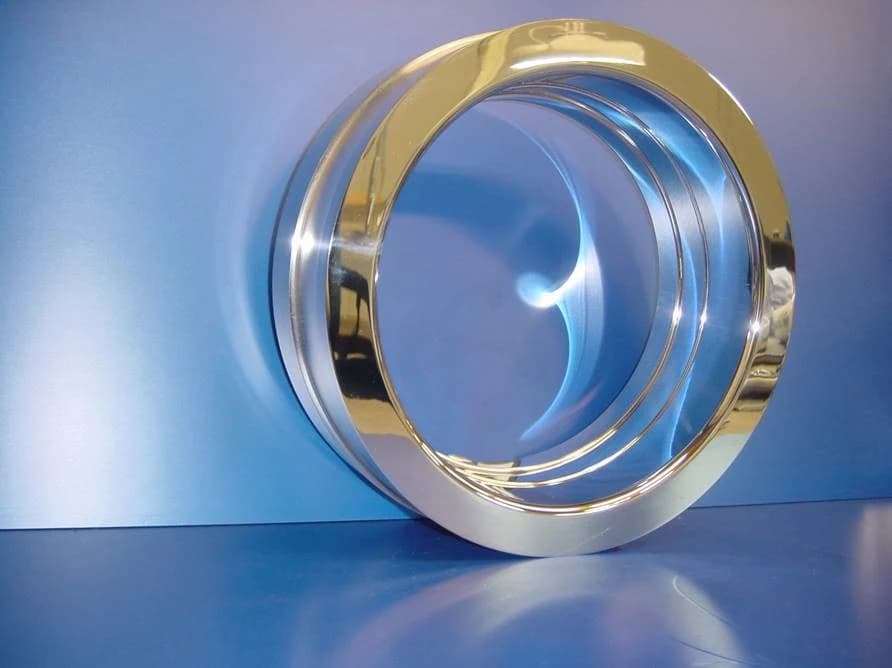
Line polishing, mirror polishing or technical polishing: at all NOVA Coating sites and at NOVA Polishing in Enger, we polish the functional surfaces of tools, moulds and components.
Polishing step by step.
Prepared surface
The forming surface has been finely pre-ground. A brush, felt and diamond paste refine it to achieve the required surface quality.
The surface takes shape …
Brush polishing. Cleaning. Felt polishing. Mirror finish.
Polishing in detail.
We offer polishing in Krefeld, Kulmbach, Maulbronn, Enger, Suzhou and Pune. We adapt the finish to your application and any subsequent coating. Your chosen site handles your enquiry.
Our services
- Line polishing
- Mirror polishing
- Technical polishing
- Mould-release polishing: polishing marks aligned with the release direction
- Specified Ra and Rz roughness, from grit 80 to a mirror finish
- Polishing from 3D data (flat surfaces only)
- Measurement of tools and moulds
- Mould surface repair service
- Surface finishing before and after coating
SURFACE QUALITY
Which level
does your surface need?
| Stage | Sample | Ra Arithmetic mean roughnessµm | Rz Mean roughness depthµm |
|---|---|---|---|
| Line polishingDirectional satin polishing marks. For forming, stamping and cutting surfaces where the functional direction matters. | |||
| K 80 | 0,92 µm | 7,76 µm | |
| K 120 | 0,94 µm | 7,87 µm | |
| K 150 | 0,58 µm | 5,06 µm | |
| K 220 | 0,45 µm | 4,11 µm | |
| K 280 | 0,41 µm | 4,14 µm | |
| K 320 | 0,28 µm | 2,93 µm | |
| K 400 | 0,19 µm | 1,74 µm | |
| Technical polishingA fine, uniform appearance with visible gloss. The usual base for PVD coatings and mould surfaces without optical requirements. | |||
| K 600 | 0,13 µm | 1,41 µm | |
| K 800 | 0,08 µm | 0,86 µm | |
| K 1000 | 0,08 µm | 0,56 µm | |
| K 1200 | 0,06 µm | 0,54 µm | |
| Mirror finishA reflective surface after additional diamond-polishing stages. For visible parts, optical components and cavities with the highest mould-release requirements. | |||
| HG | 0,06 µm | 0,36 µm | |
Indicative values measured on a tool-steel reference plate across the polishing direction. On actual workpieces, values depend on steel and geometry and are checked separately.
Discuss your polishing requirements
Tell us the functional surfaces, material and required surface quality. Together, we determine the right finish.
Contact a location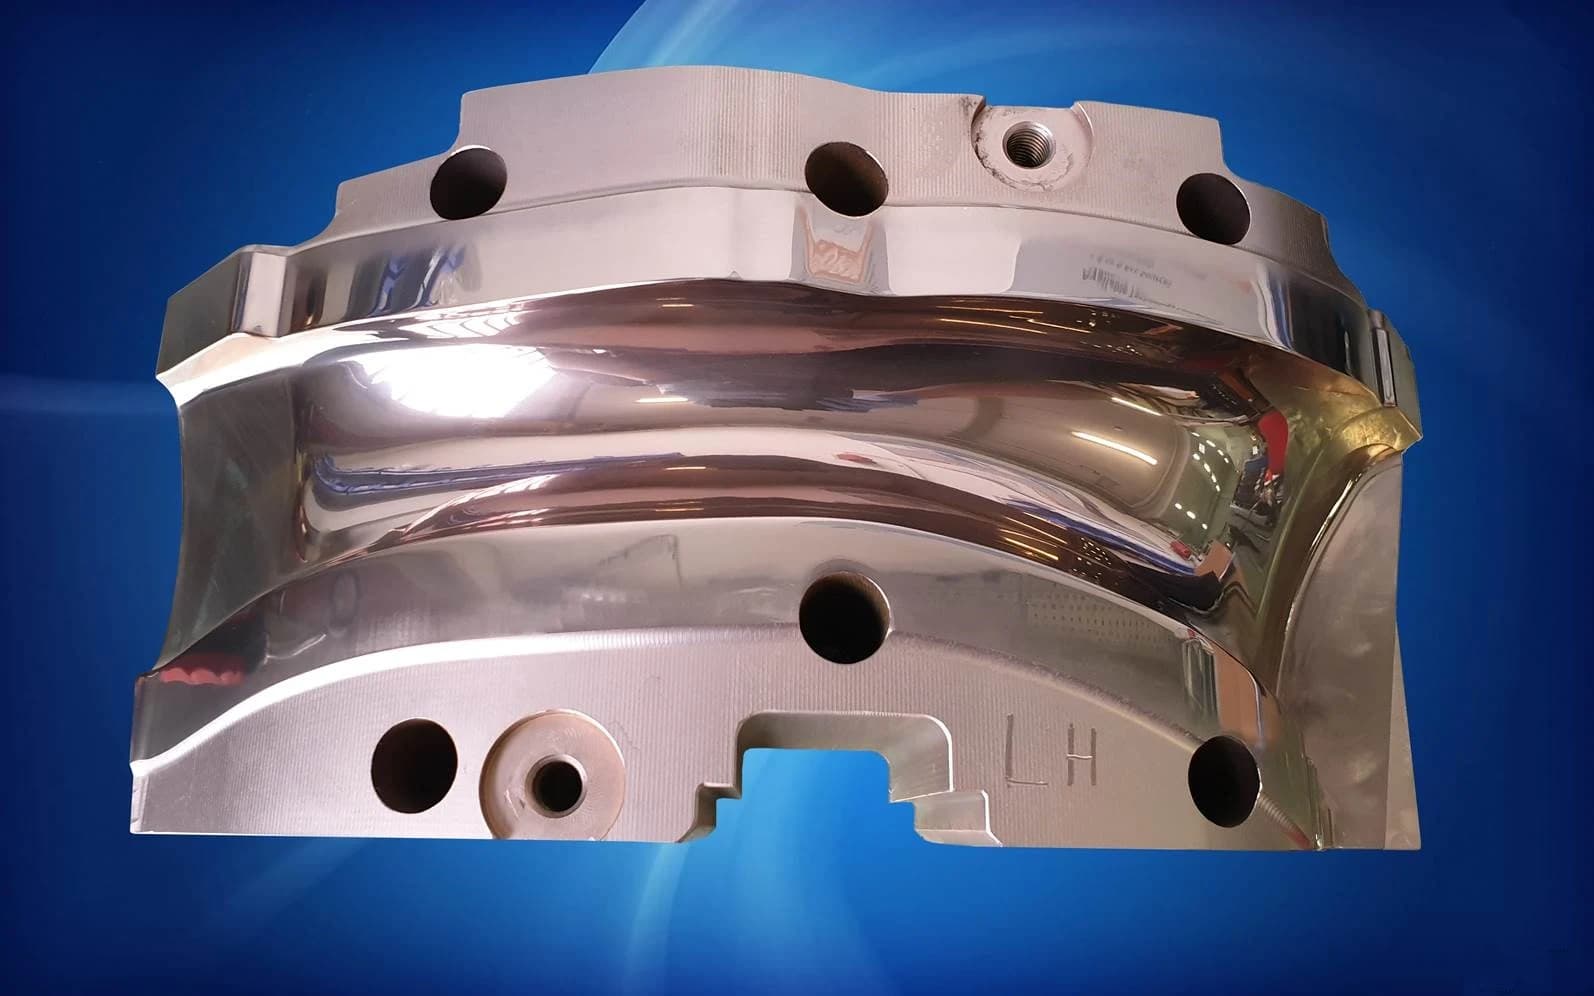
Polished forming die.
Polished by NOVA Coating and coated with MULTINOVA PLUS for forming S420 sheet metal.
Read the MULTINOVA PLUS case studyPLUS is used for stamping, forming and die casting. Through-hardened tool steels with a tempering temperature above 500 °C are required.
THE NEXT STEP