TECHNOLOGY & COATING SYSTEMS

The right coating. Down to the detail.

All coatings for tools and components: as a Nova coating service or as a coating programme for your Asgard or Apex system.

1 COATING SYSTEMS · EXPAND FOR DETAILS

Labels explained
PLUS

PLUS means additional plasma nitriding before PVD coating (duplex). It supports the PVD coating on through-hardened tool steel. nitriding hardness depth: 0.02–0.05 mm. Depending on the system, PLUS is optional or always included. PLUS is used for stamping, forming and die casting. Through-hardened tool steels with a tempering temperature above 500 °C are required.

M-Guard optional
Additional diffusion treatment for plastics applications. Can be combined with the marked PVD coatings.
F-series available
Also available as a separate F variant for specific testing and approval requirements. See the coating details for application areas.
MP-CUTAlTiCrN-basedAvailable as a Nova serviceHardness in HV: 3300 ± 400Coating thickness in micrometres: 1–3Maximum operating temperature in degrees Celsius: 1100
Composition
AlTiCrN-based
Hardness
3300 ± 400 HV
Coating thickness
1–3 µm
Max. operating temperature
1100 °C
Coating temperature
450–480 °C
Coefficient of friction
0.5
Colour
Anthracite
Plus option / duplex
Not specified
Finishing as required
Available

Recommended applications according to the coating overview

  • Machining

Technical guidance based on the NOVA coating overview and Apex datasheets. Properties depend on the system and application. We confirm suitability and current specifications with you.

Open the Nova service portfolio as an image ↗
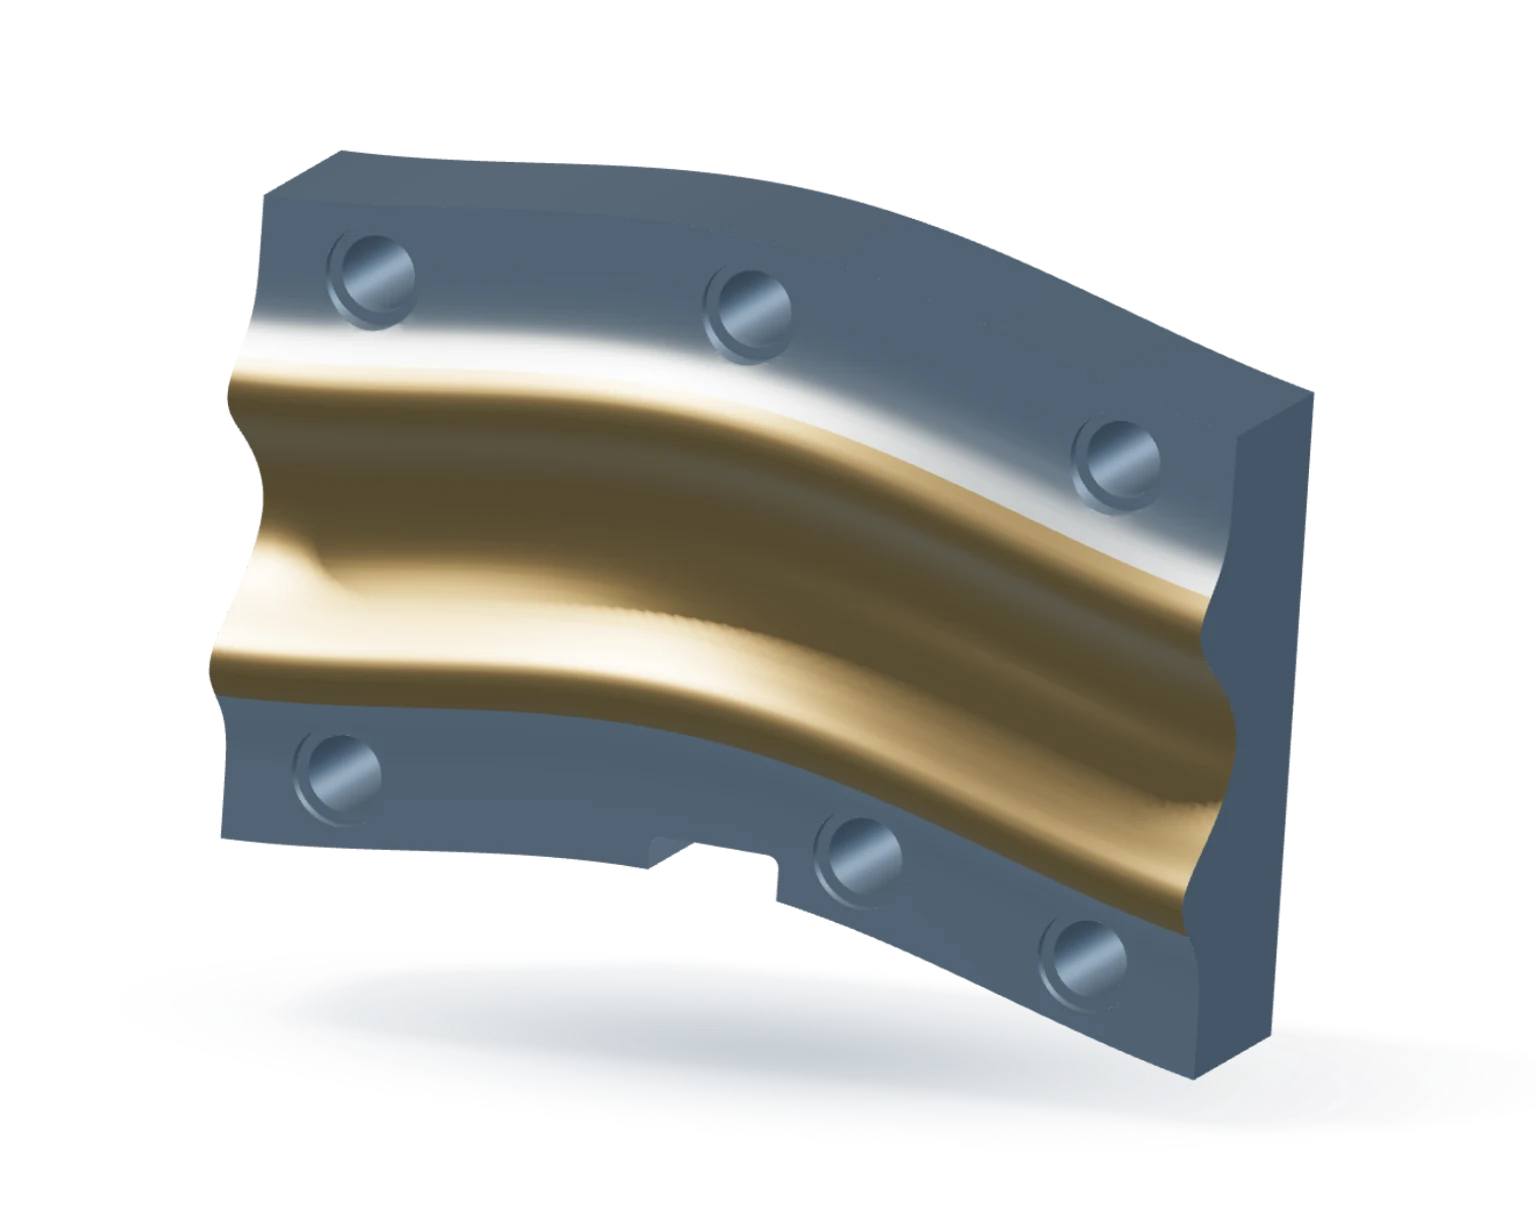
See how our coatings look.

Schematic forming tool with six through-holes and a golden functional surface
Forming tool with polished functional surface

Schematic model based on an original NOVA tool.

Schematic illustration. Colours may vary.

Why a coating pays off.

Material efficiency

A longer-lasting tool replaces several tools. This reduces both the number of tools in circulation and the steel that needs to be cast, machined and transported.

Longer service life

The coating takes the wear, not the tool. If geometry is preserved, the tool can be stripped, repolished and recoated, returning to production instead of being replaced.

Predictable maintenance

Uniform wear makes replacement intervals predictable. Maintenance can be scheduled rather than forced, reducing unexpected downtime.

THE NEXT STEP

Coating service or your own system?

We will advise you on the right coating and how to obtain it.

Request advice