60 HRC
Hard machining of 1.2379in the documented NOVA application report
FROM MILLING CUT TO CUTTING EDGE
01 / The tool
Milling hardened tool steel.
An end mill with ALSINOVA PRO machines 1.2379 at 60 HRC.
Technical data & application report
- Tool
- End mill · Ø 6 mm
- Coating
- ALSINOVA PRO with finishing
- Workpiece
- 1.2379 · 60 HRC
- Cutting speed vc
- 150 m/min
- Feed per tooth fz
- 0.04 mm/tooth
- Radial engagement ae / cutting depth ap
- 6 mm / 0,15 mm
- Cooling
- Dry · compressed air
- NOVA wear after 50 m
- 0.066 mm
- Competitor images
- after 36.8 m
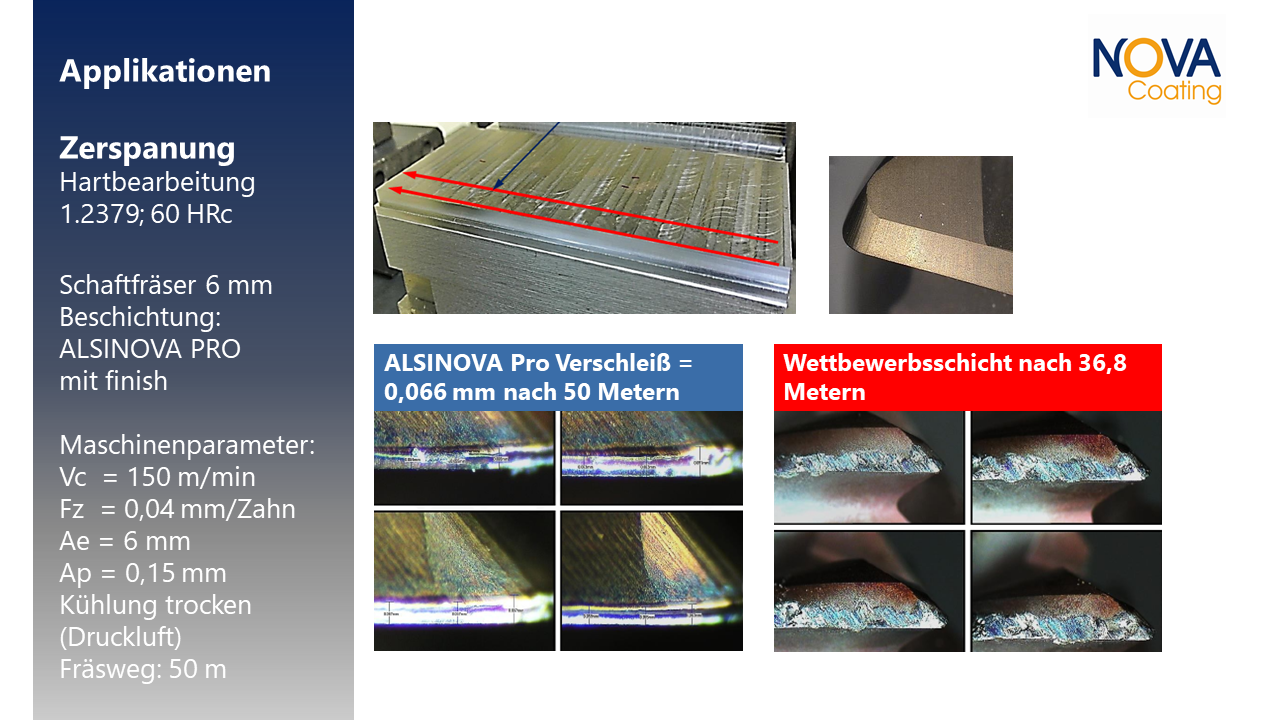
Tool geometry, milling distance and movement are schematic. Wear zones illustrate the photographic findings qualitatively; they are not measured 3D reconstructions. The 0.066 mm figure denotes documented wear, not coating thickness. The different imaging times do not establish a general tool-life improvement.
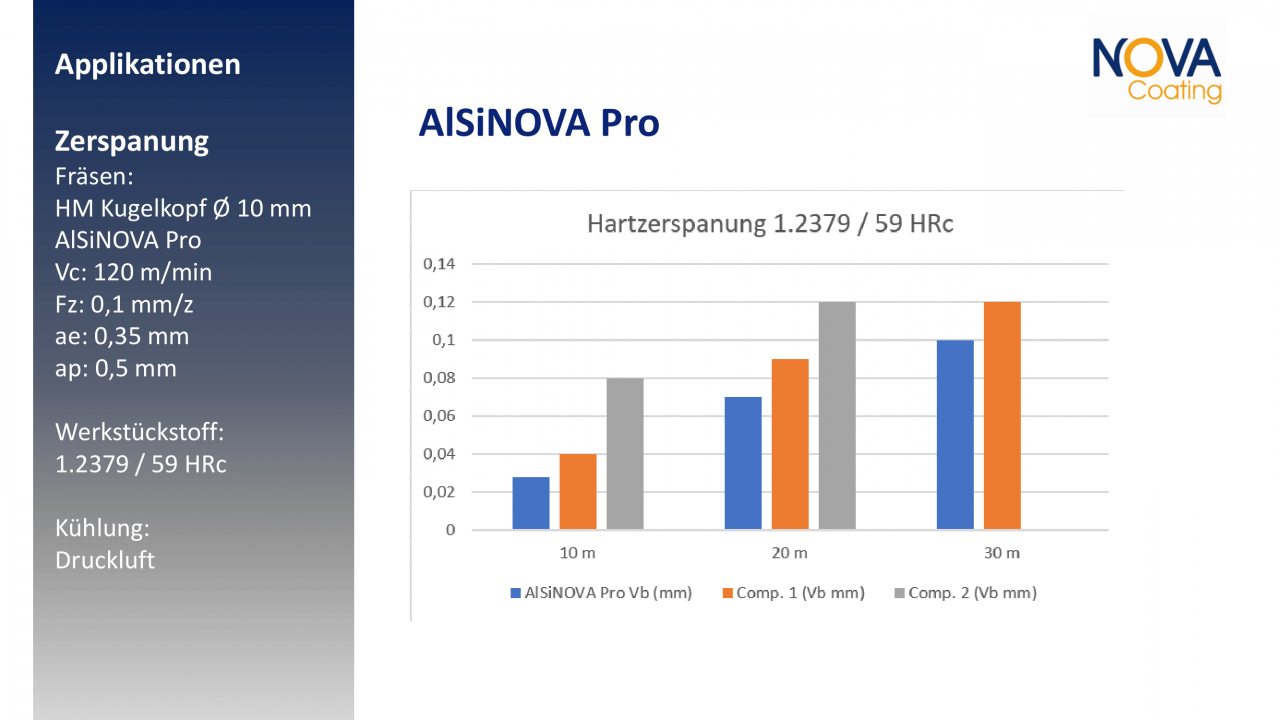
Further trial: Ø 10 mm ball-nose cutter
A separate trial under different machining conditions. Its values are not part of the animation.